
CUSTOM CONVEYOR SYSTEMS FOR MATERIAL FLOW AND PACKAGING OPERATIONS
Custom conveyor systems support efficient product flow and packaging operations, enabling reliable movement of containers and materials across production lines.
Please view our extensive case study catalog to learn how Trotter can help you solve your engineering needs.
Custom conveyor systems support efficient product flow and packaging operations, enabling reliable movement of containers and materials across production lines.
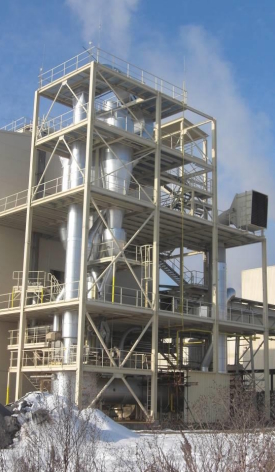
Ring and flash dryers handle fine and heat-sensitive materials with short residence time, enabling high-capacity drying and energy-efficient operation in industrial processes.
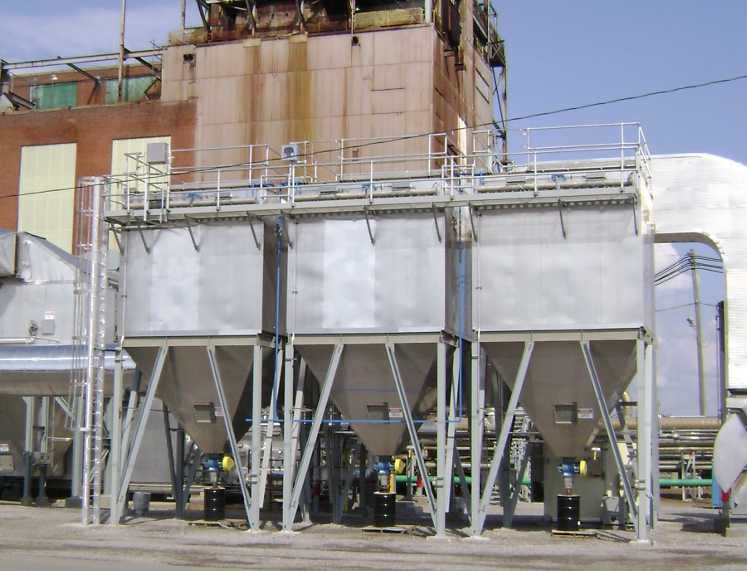
Industrial dust collection systems improve air quality and process reliability by capturing particulate emissions and enabling safe, compliant plant operation.

Security screening systems remove impurities and break agglomerates in bulk materials, supporting product quality and consistent downstream processing.
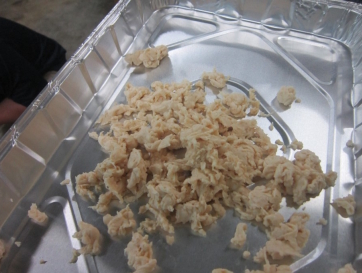
Continuous processing hydrates, emulsifies, and texturizes plant proteins, improving consistency and efficiency in meat analog production with integrated thermal processing.

Maximize wood fiber recovery and eliminate waste in high-speed sawmilling lines. Advanced gyratory screening technology allows for higher log feeding speeds while maintaining strict chip specifications and protecting your bottom line.

Continuous processing of modified asphalt rapidly disperses additives, reducing energy consumption and processing time while improving product consistency in asphalt applications.
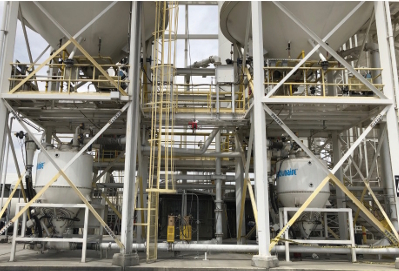
Streamline fly ash production by weighing, batching, and blending in a single pneumatic unit. This semi-dense conveying solution simplifies maintenance and ensures continuous operation with simultaneous dual-conveyor processing.
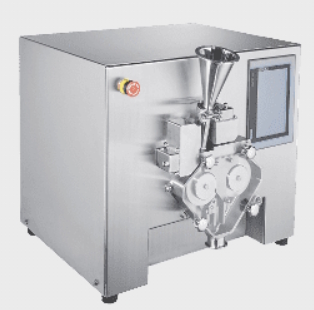
Roll compaction systems improve powder flow and uniformity by converting fine materials into granules, enhancing downstream processing and tablet manufacturing efficiency.

Optimize cocoa processing with high-efficiency sifting designed to handle fatty, heat-sensitive materials. These custom systems prevent screen blinding and ensure consistent particle sizing for premium chocolate production.
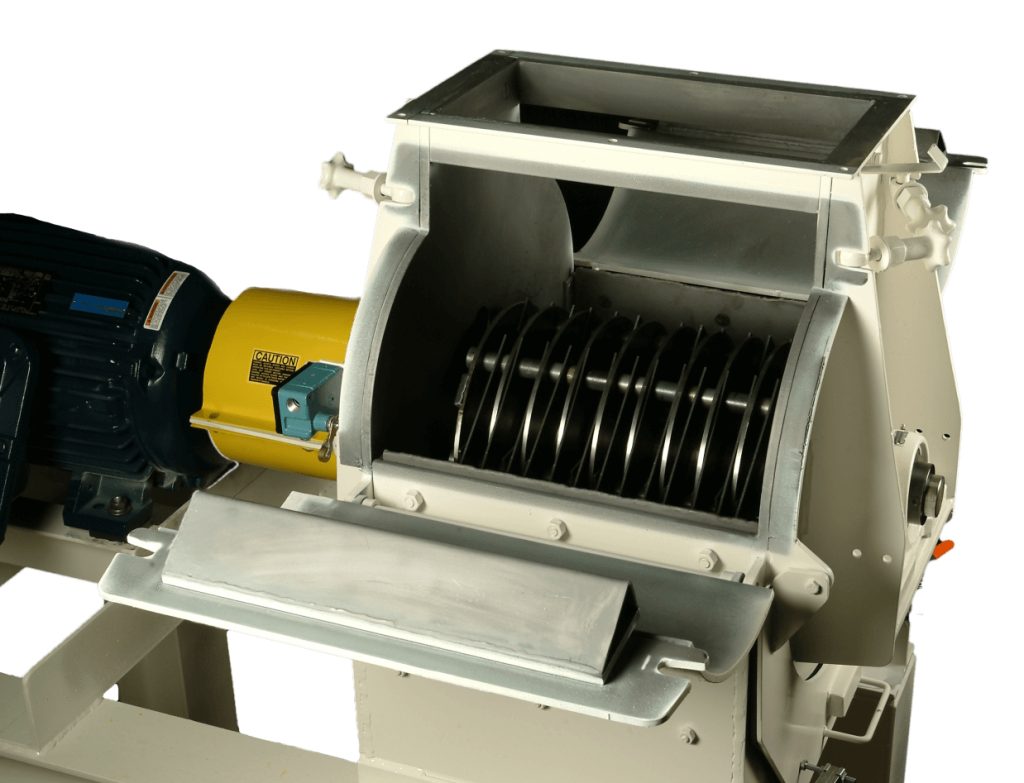
Optimize soy flake and meal processing. A Mega Mill and M-Series Fine Grinder solve challenges with fatty soy meal maintenance and high-fiber flake shearing.
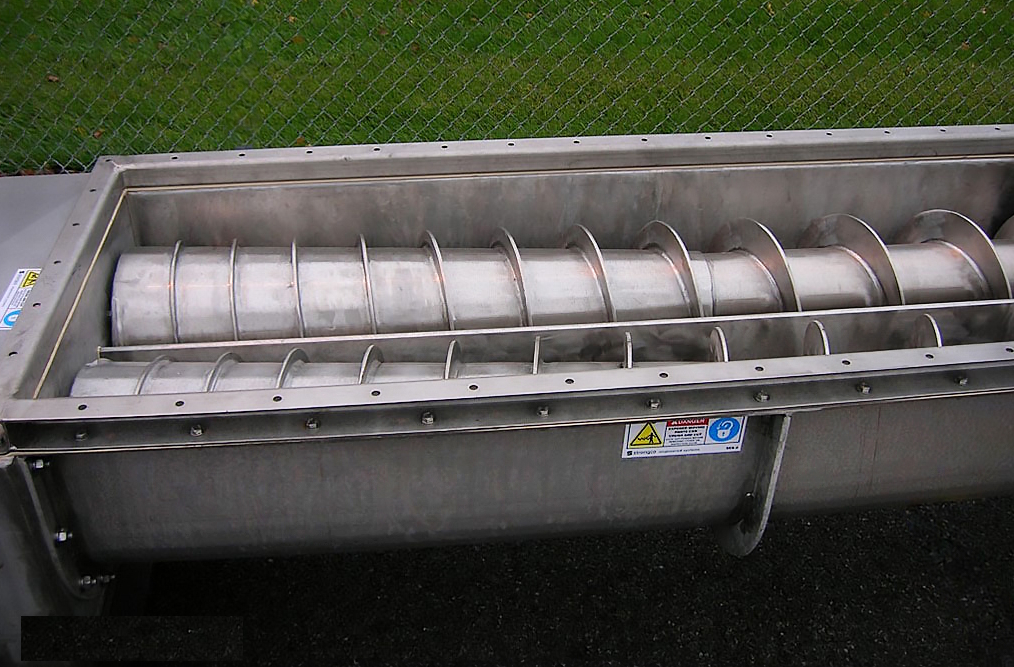
Mass flow screw feeders provide uniform material discharge from hoppers, supporting consistent flow, controlled feed rates, and reliable bulk solids handling.
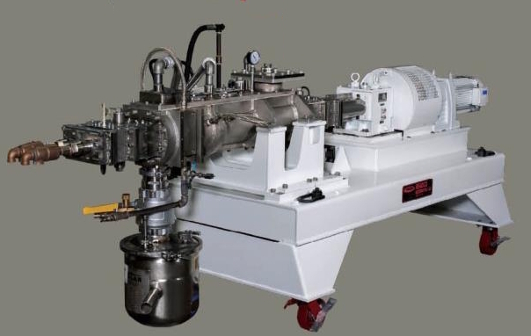
Continuous processing removes solvent from SBR slurry under vacuum, reducing volatiles and improving product quality while minimizing fouling and energy consumption.
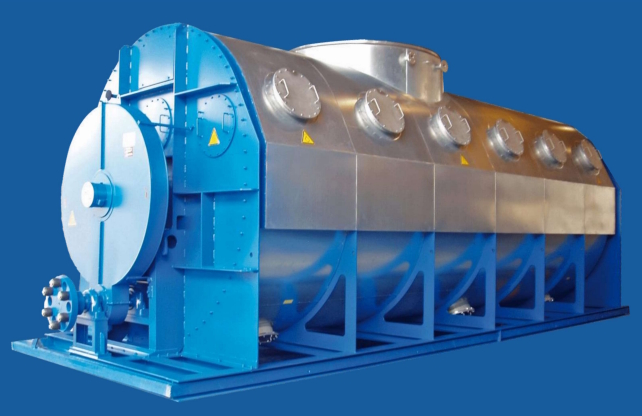
Indirect steam tube bundle dryer improves drying efficiency, reduces emissions, and enables high-capacity evaporation with energy recovery up to 90%.
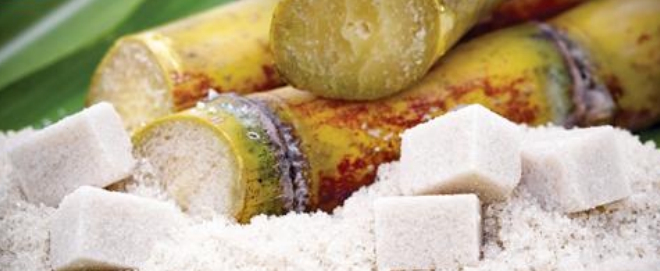
Sugar screening systems improve product uniformity and recovery by separating grades efficiently, increasing yield, and reducing downtime in high-capacity processing operations.
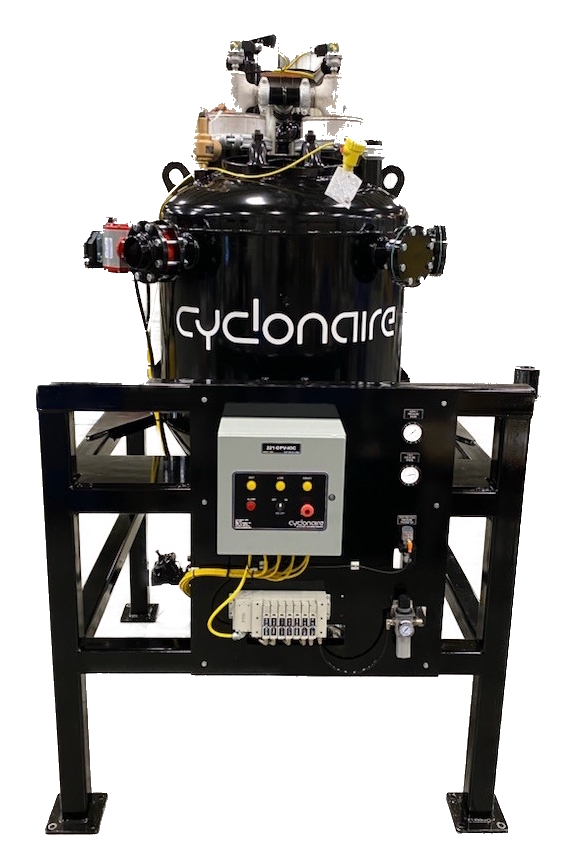
Eliminate cross-contamination and material degradation in your rubber compounding process. This dense-phase pneumatic conveying system replaces high-maintenance bucket elevators with a closed-loop design that ensures material grade integrity and efficient dust recovery for friable carbon black pellets.
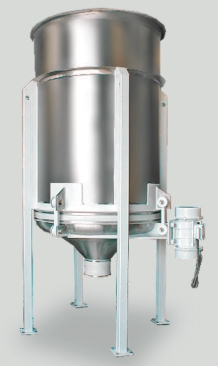
Inconsistent urea flow to melter causes buildup and downtime until live bottom bin and screw feeder deliver precise, continuous feed rates.
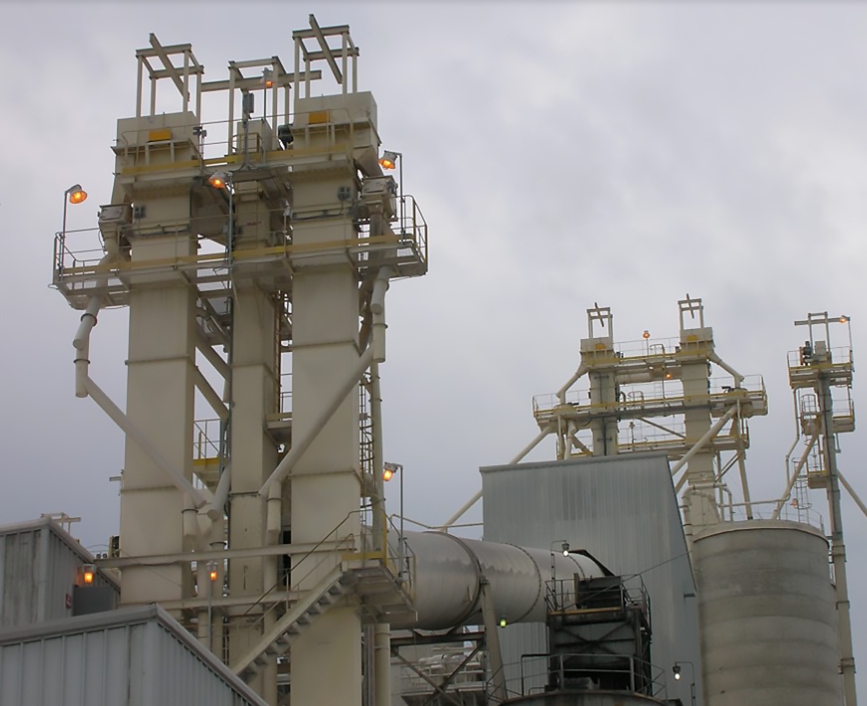
Bucket elevator design and selection impact capacity, safety, and material handling performance, with speed, discharge type, and construction determining reliability.
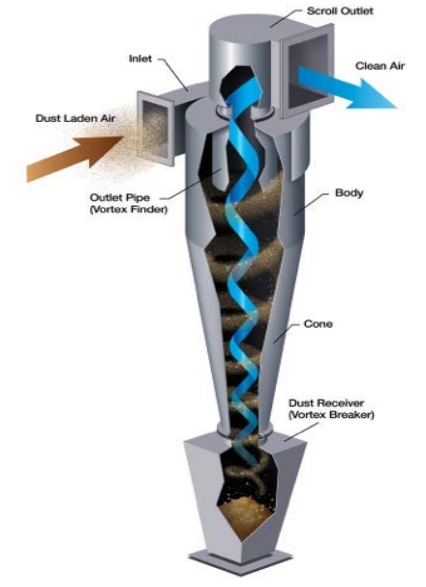
Cyclone separator design improves particulate removal by balancing efficiency, pressure drop, and particle size, reducing emissions and protecting downstream equipment.

Seed cleaning and sizing systems separate fines and splits from grains using gyratory screening, improving product quality, increasing throughput, and reducing operating costs.
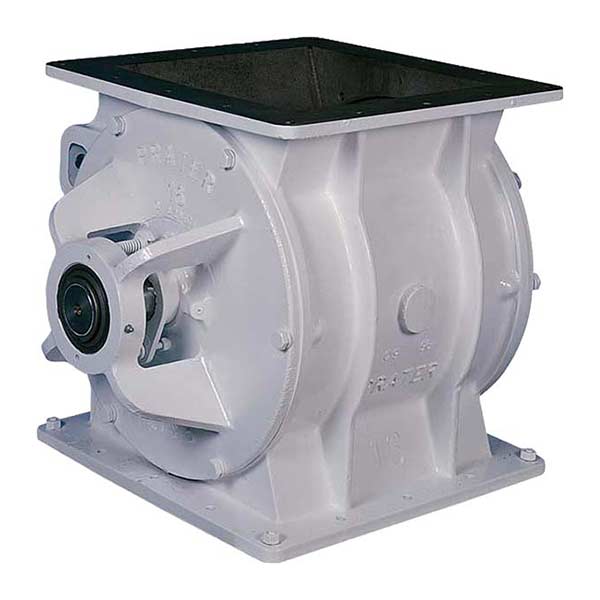
Enhance vinyl flooring production with specialized pneumatic conveying and material handling. Our systems utilize heavy-duty rotary valves and high-efficiency dust collection to ensure consistent, contaminant-free powder flow.