
DUST RECLAIM SYSTEM IMPROVES SILO AIR QUALITY AND MATERIAL RECOVERY
Dust reclaims system returns captured silo dust automatically, improving air quality, reducing waste, and eliminating manual handling in bulk material operations.

Dust reclaims system returns captured silo dust automatically, improving air quality, reducing waste, and eliminating manual handling in bulk material operations.
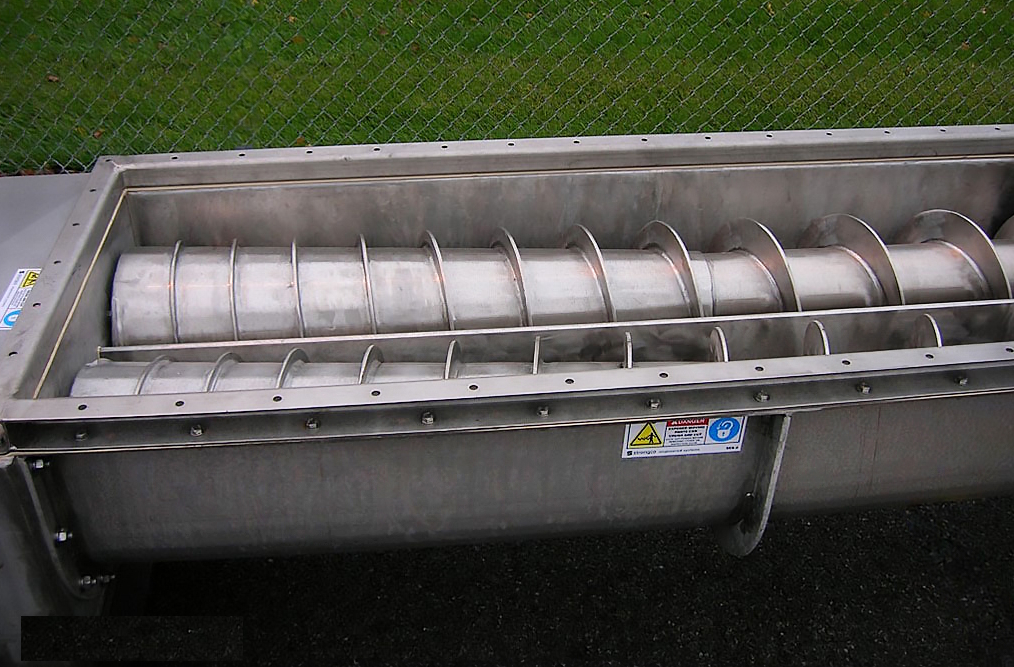
Mass flow screw feeders provide uniform material discharge from hoppers, supporting consistent flow, controlled feed rates, and reliable bulk solids handling.
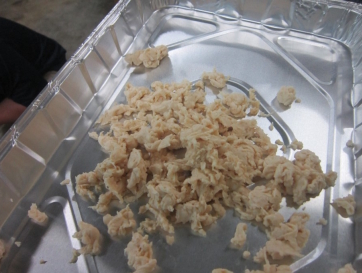
Continuous processing hydrates, emulsifies, and texturizes plant proteins, improving consistency and efficiency in meat analog production with integrated thermal processing.
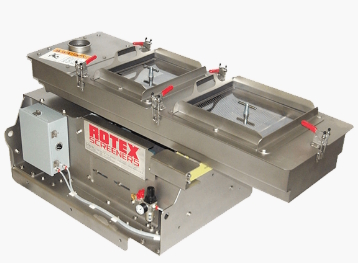
Plastic pellet screening systems remove fines and elongated particles, improving product quality, increasing recovery, and supporting efficient compounding operations.
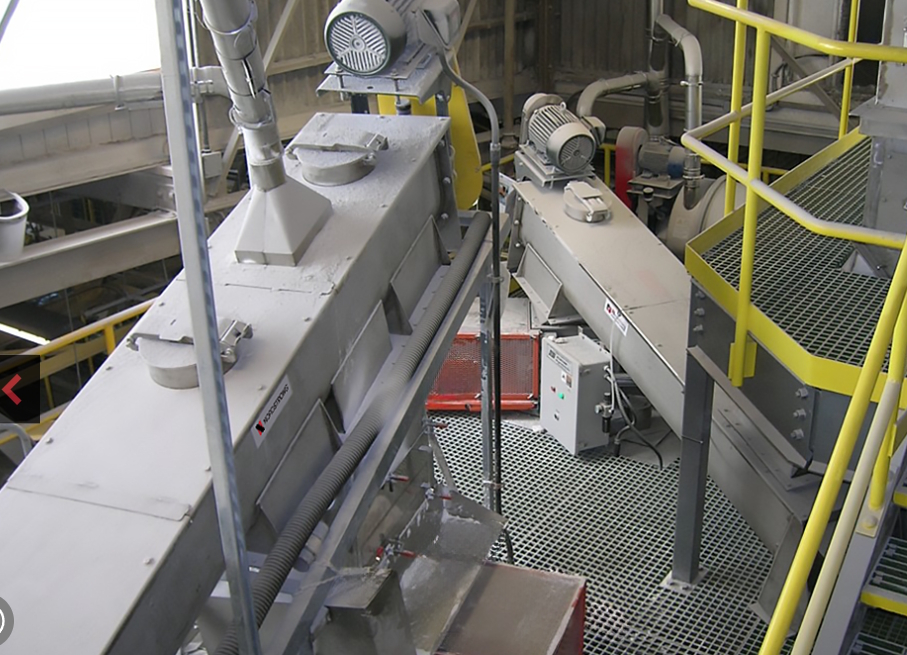
Screw conveyors provide efficient enclosed transport of bulk materials, enabling reliable flow control and flexible layout in industrial material handling systems.
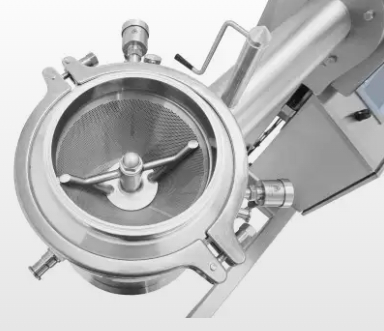
Conical milling systems improve particle size control in pharmaceutical processing, enhancing mixing, drying efficiency, and final product consistency.
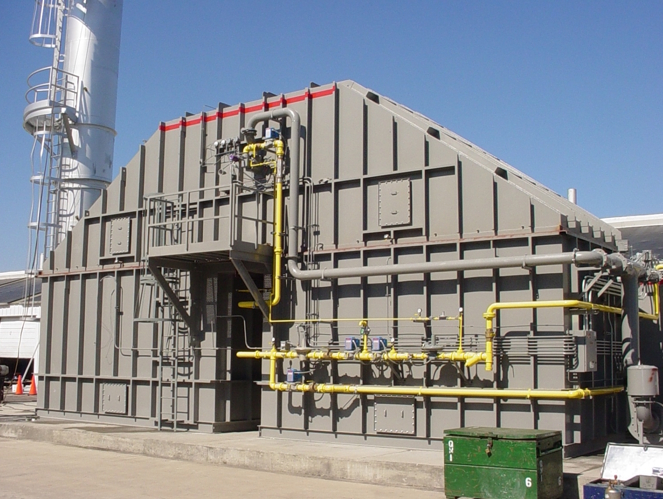
Regenerative thermal oxidizers destroy VOC emissions while recovering up to 95% heat, lowering fuel costs and enabling energy-efficient air pollution control.
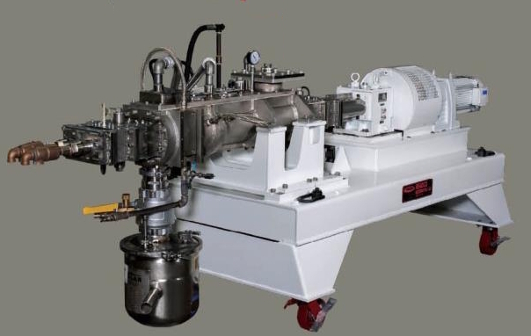
Continuous processing removes solvent from SBR slurry under vacuum, reducing volatiles and improving product quality while minimizing fouling and energy consumption.

Continuous processing rapidly disperses powders into high‑viscosity resin, improving consistency and reducing cleanup time in carbon fiber prepreg manufacturing.

Security screening systems remove impurities and break agglomerates in bulk materials, supporting product quality and consistent downstream processing.

Screening systems for recyclable materials separate fines, metals, and plastics, improving recovery rates, reducing waste, and increasing efficiency in high-volume recycling operations.
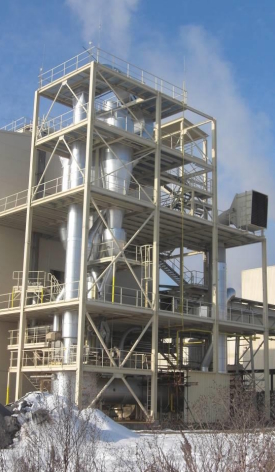
Ring and flash dryers handle fine and heat-sensitive materials with short residence time, enabling high-capacity drying and energy-efficient operation in industrial processes.
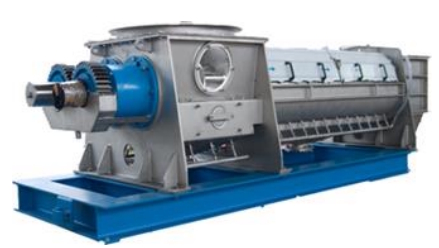
Screw press dewatering systems remove moisture from biomass and industrial materials, lowering energy demand and improving downstream drying efficiency.
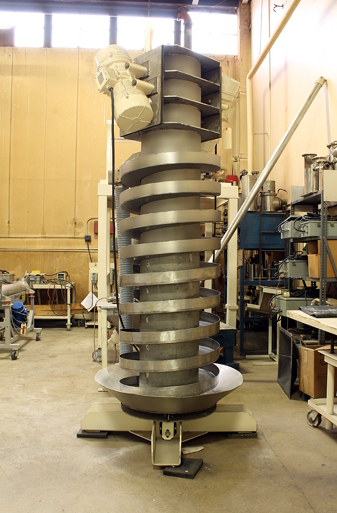
Spiral conveyors elevate bulk materials vertically while enabling cooling, drying, or heating, improving plant layout efficiency and reducing equipment footprint.

Air classifiers separate particles by size and density using adjustable airflow and rotor speed, improving product quality and efficiency in bulk material processing.

Industrial screening systems separate fines, hulls, and meal in soybean processing, improving product quality, reducing wear, and increasing efficiency across high-capacity operations.
Sugar screening systems improve product uniformity and recovery by separating grades efficiently, increasing yield, and reducing downtime in high-capacity processing operations.
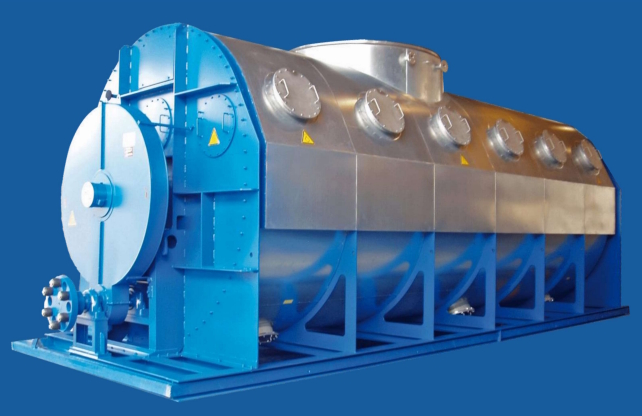
Indirect steam tube bundle dryer improves drying efficiency, reduces emissions, and enables high-capacity evaporation with energy recovery up to 90%.
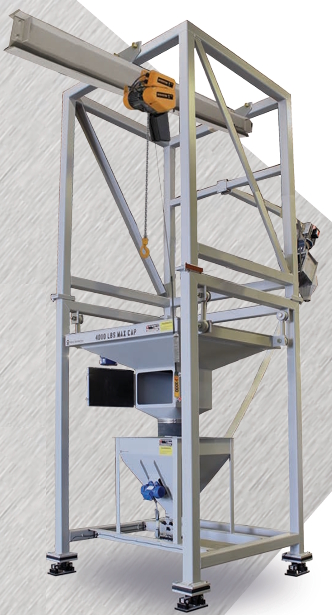
Bulk bag unloading systems provide safe, dust-free discharge of dry materials, improving handling efficiency, flow control, and integration with downstream processing equipment.
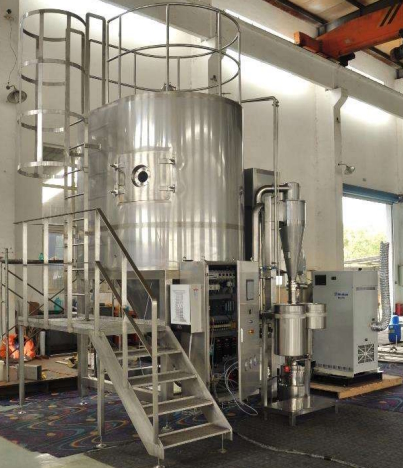
Spray drying converts liquid feed into powder using atomization and hot air, enabling controlled particle formation and high-capacity drying across food and chemical processing.

Continuous processing maintains tight moisture tolerances during powder conditioning, enabling uniform dispersion and direct feeding to downstream production equipment.